Ammonia Refrigeration System
Ammonia Refrigeration System Manufacturers in India
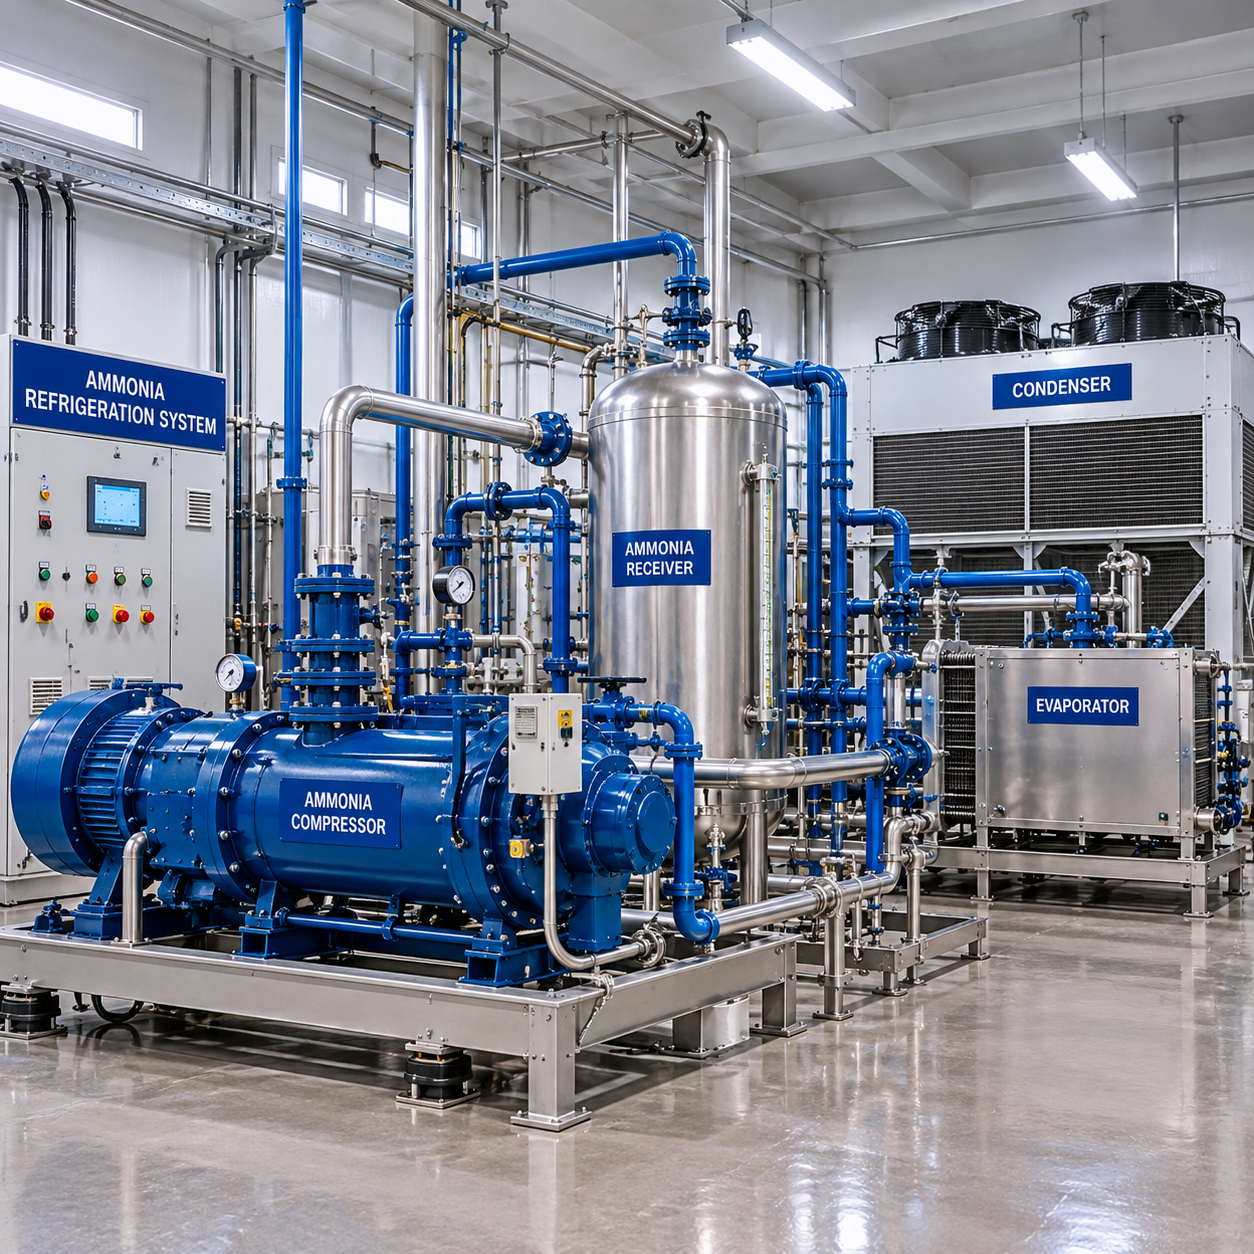
H. A. Engineering is trusted Ammonia Refrigeration System Manufacturers and Suppliers in India. We understand that industries such as cold storage, dairy processing, food manufacturing, ice plants, and logistics require dependable refrigeration solutions capable of maintaining precise temperature control while minimizing operating costs.
We develop advanced Industrial Ammonia Refrigeration Systems using high-quality components, energy-efficient compressors, and intelligent control systems. Ammonia (NH₃) is one of the most effective natural refrigerants available today, offering excellent thermodynamic properties, low environmental impact, and superior heat transfer performance. Our systems are engineered to provide consistent cooling even under demanding operating conditions.
With years of engineering expertise, we offer customized Cold Storage Ammonia Refrigeration Systems, ammonia chillers, ammonia glycol refrigeration systems, and low-charge ammonia solutions. We focus on delivering systems that ensure operational safety, energy savings, long equipment life, and compliance with industrial refrigeration standards.
What is an Ammonia Refrigeration System?
An Ammonia Refrigeration System is an industrial cooling system that uses ammonia (NH₃) as a refrigerant to remove heat from a designated area and maintain low temperatures. Due to its excellent cooling efficiency and environmentally friendly characteristics, ammonia is widely used in cold storage facilities, food processing plants, dairy industries, ice manufacturing units, and large-scale warehouses.
The system operates through a refrigeration cycle involving compression, condensation, expansion, and evaporation. Ammonia absorbs heat from the process area and transfers it outside, creating a controlled cooling environment. Because of its high energy efficiency, ammonia refrigeration remains a preferred solution for large industrial cooling applications worldwide.
Working Principle of Ammonia Refrigeration System
The working principle of an ammonia refrigeration system is based on the vapor compression refrigeration cycle.
- The compressor compresses low-pressure ammonia vapor into high-pressure vapor.
- The condenser removes heat and converts the vapor into liquid ammonia.
- The expansion valve reduces pressure and temperature of the liquid refrigerant.
- The evaporator absorbs heat from the cooling area, causing ammonia to evaporate.
- The vapor returns to the compressor, and the cycle repeats continuously.
This continuous process ensures effective cooling, temperature stability, and energy-efficient operation for industrial refrigeration applications.
Test Cases of Ammonia Refrigeration System
As a trusted Ammonia Refrigeration System Manufacturers in India, we serve businesses across various industries that meet professional visual communication requirements.
| Test Parameter | Testing Method | Expected Result | Industry Standard | Status |
|---|---|---|---|---|
| Cooling Capacity Test | Load Simulation | Specified TR Output | Industrial Standard | Pass |
| Pressure Leak Test | Nitrogen Pressure Test | No Leakage | Safety Compliance | Pass |
| Compressor Performance Test | Operational Run Test | Stable Operation | Manufacturer Standard | Pass |
| Temperature Control Test | Sensor Verification | Accurate Cooling | Quality Standard | Pass |
| Safety System Test | Alarm & Shutdown Check | Proper Activation | Safety Regulations | Pass |
Features of Ammonia Refrigeration System
As Ammonia Refrigeration System Suppliers in India, we have advanced features that ensure high precision, durability, and consistent performance.
- High Cooling Efficiency: We design systems that provide exceptional heat transfer performance, ensuring faster and more efficient cooling. This improves productivity while reducing energy consumption.
- Energy-Efficient Operation: Our ammonia refrigeration plants are engineered to optimize power usage and lower operating expenses. This helps industries achieve significant long-term cost savings.
- Industrial-Grade Construction: We manufacture systems using robust materials and premium components for reliable performance. This ensures durability even in demanding industrial environments.
- Advanced Safety Controls: Our systems incorporate monitoring devices, safety valves, and automated controls. These features enhance operational safety and regulatory compliance.
- Customizable Capacity Range: We offer solutions ranging from small ammonia refrigeration systems to large industrial plants. This flexibility allows us to meet diverse cooling requirements.
Benefits of Ammonia Refrigeration System
As Ammonia Refrigeration System Manufacturers in India, our products provide several benefits including consistent quality, smooth finish, and long service life.
- Lower Energy Costs: Ammonia's superior thermodynamic properties enable efficient heat transfer and reduced power consumption. This lowers overall operating costs for industrial facilities.
- Environmentally Friendly Solution: Ammonia is a natural refrigerant with zero ozone depletion potential. It supports sustainable refrigeration practices and environmental compliance.
- Long Service Life: Our systems are designed for durability and reliable operation over extended periods. This reduces maintenance frequency and replacement expenses.
- Superior Cooling Performance: The refrigeration cycle delivers consistent and effective cooling across large facilities. This ensures product quality and temperature stability.
- High Return on Investment: Reduced energy usage and dependable operation contribute to significant long-term savings. Industries benefit from improved operational efficiency and profitability.
Applications of Ammonia Refrigeration System
As Ammonia Refrigeration System Suppliers in India, our all types are used in various types of industrial sectors such as:
- Cold Storage Facilities: We provide ammonia refrigeration systems for maintaining low temperatures in cold storage warehouses. These systems preserve product freshness and quality.
- Dairy Processing Plants: Our refrigeration solutions support milk chilling, butter production, and dairy storage operations. They help maintain product safety and processing efficiency.
- Food Processing Industry: We supply cooling systems for food manufacturing facilities requiring precise temperature control. This improves product consistency and shelf life.
- Ice Manufacturing Plants: Ammonia refrigeration is widely used in commercial ice production operations. It ensures efficient freezing and high production capacity.
- Frozen Food Storage: Our systems maintain stable temperatures for frozen food warehouses and distribution centers. This protects products from spoilage and quality loss.
- Beverage Manufacturing Units: We offer refrigeration solutions for beverage cooling and processing applications. These systems support efficient production and storage operations.
- Meat and Poultry Processing: Our ammonia refrigeration plants provide reliable cooling for meat processing facilities. This ensures compliance with food safety requirements.
- Pharmaceutical Storage: We design systems for pharmaceutical warehouses requiring controlled temperature environments. This helps preserve product integrity and effectiveness.
- Ice Rinks and Recreational Facilities: Ammonia refrigeration systems are used for maintaining ice surfaces in skating arenas. They provide consistent cooling performance throughout operation.
- Logistics and Distribution Centers: We deliver warehouse ammonia refrigeration systems for temperature-sensitive inventory. These solutions support efficient supply chain management.
Why Choose Us?
- Industry Expertise: We possess extensive experience in designing and manufacturing industrial refrigeration solutions. Our expertise ensures reliable and customized system performance.
- Quality Manufacturing: We use premium-grade materials and advanced engineering practices in every project. This guarantees durability, efficiency, and operational reliability.
- Customized Solutions: We design refrigeration systems according to specific industry requirements and capacities. This ensures optimal performance for every application.
- Technical Support: Our dedicated support team assists with installation, maintenance, and operational guidance. We help maximize system efficiency and uptime.
- Competitive Pricing: We offer cost-effective ammonia refrigeration plants without compromising quality. This provides excellent value and long-term investment benefits.
Choose H. A. Engineering is leading Ammonia Refrigeration System Manufacturers and Suppliers in India. We are committed to delivering advanced Ammonia Refrigeration Systems that combine efficiency, reliability, and safety. Our industrial refrigeration solutions are engineered to meet the demanding cooling requirements of modern industries while reducing energy consumption and operating costs. We continuously focus on innovation, quality manufacturing, and customer satisfaction to provide refrigeration systems that deliver long-term performance. Contact Us For More Details.
FAQs
An ammonia refrigeration system uses ammonia as a refrigerant to provide efficient industrial cooling for various applications.
Ammonia offers excellent cooling efficiency, low environmental impact, and cost-effective operation compared to many synthetic refrigerants.
Yes, when designed and maintained properly with safety controls and monitoring systems, ammonia refrigeration is highly safe and reliable.
Cold storage, dairy processing, food manufacturing, pharmaceuticals, ice plants, and logistics facilities commonly use ammonia refrigeration systems.
Ammonia refrigeration systems are available in various capacities, ranging from small industrial units to large-scale plants exceeding several hundred TR.