Cold Room
Cold Room Manufacturers in India
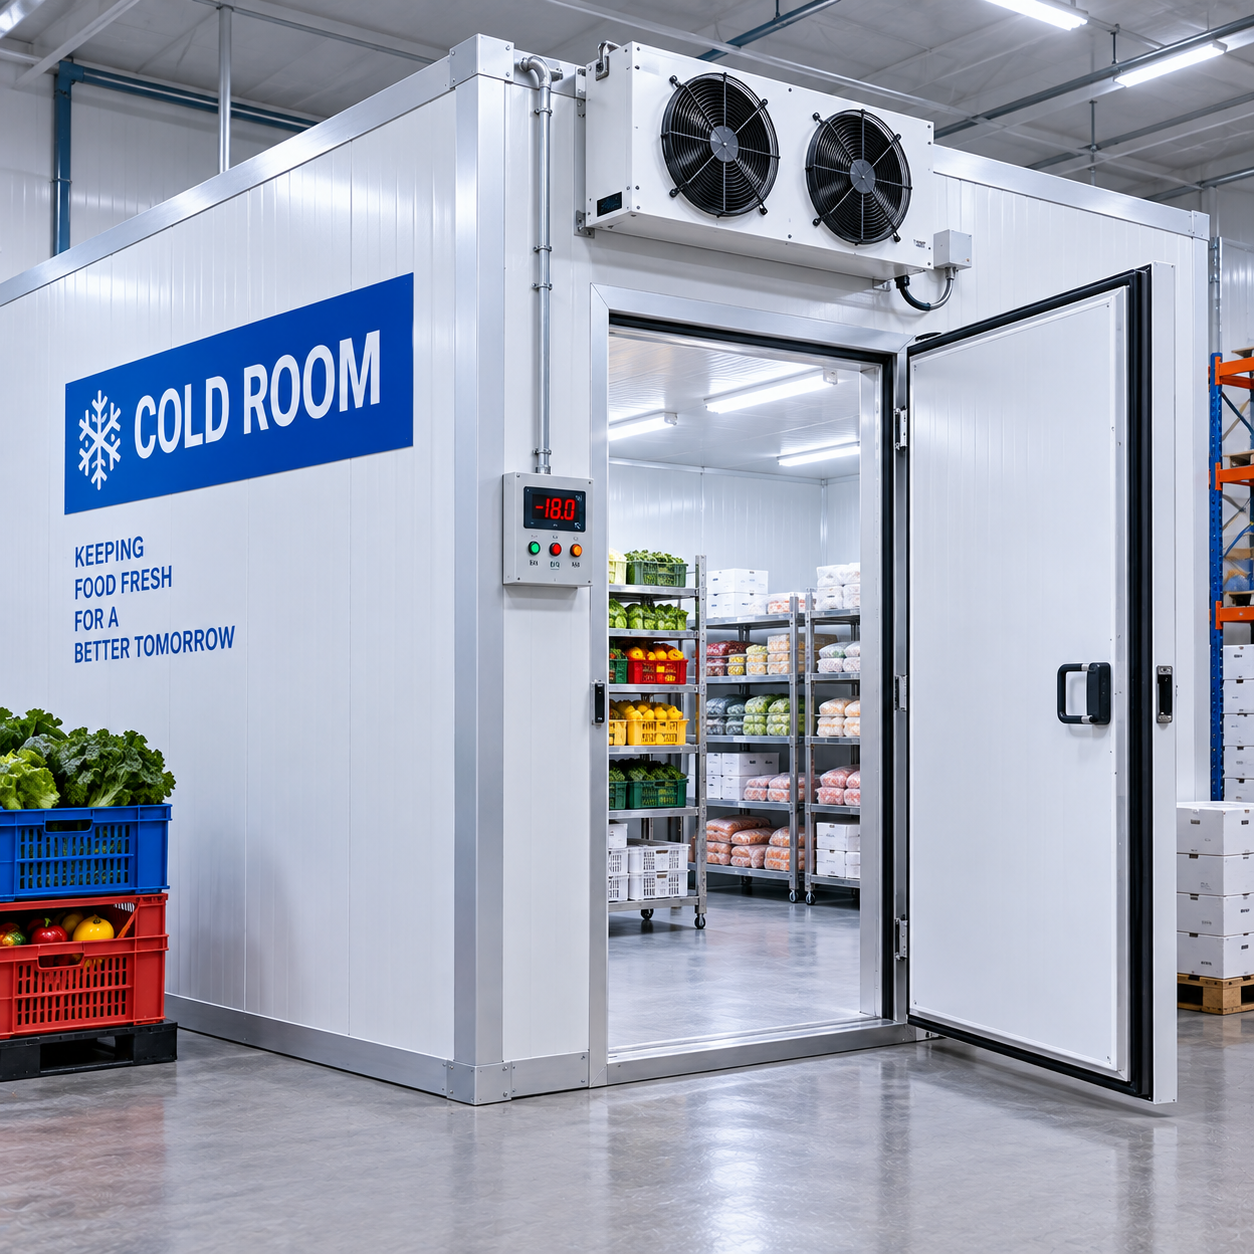
H. A. Engineering is leading Cold Room Manufacturers and Suppliers in India. Our Cold Rooms are designed to provide controlled storage environments for food products, pharmaceuticals, beverages, agricultural produce, and industrial materials. By combining advanced refrigeration technology with high-performance insulation, these systems help businesses protect inventory while ensuring compliance with industry standards.
As storage requirements continue to evolve across different sectors, modern cold room solutions have become an indispensable part of supply chain management. Our cold rooms are engineered to deliver reliable cooling performance, energy efficiency, and long-term operational durability.
We offer a complete range of Modular Cold Rooms, Walk-In Cold Storage Rooms, PUF Panel Cold Rooms, and Industrial Cold Rooms that can be customized according to capacity, temperature range, and application requirements. From restaurants and hotels to pharmaceutical companies and cold storage warehouses, our solutions support efficient and dependable temperature-controlled storage.
What Is a Cold Room and How Does It Work?
A Cold Room is a temperature-controlled storage space designed to preserve products that require cooling or freezing conditions. Unlike standard refrigeration units, cold rooms provide larger storage capacities and can be customized to accommodate different products, storage volumes, and temperature requirements.
The system works by using refrigeration equipment that continuously removes heat from the storage area and maintains a predetermined temperature range. Insulated walls, ceilings, and floors—typically constructed using PUF Panels—help minimize heat transfer and improve energy efficiency. Temperature sensors and control systems continuously monitor conditions to ensure product safety and storage consistency.
Depending on the application, cold rooms can operate at positive temperatures for fresh produce, dairy products, and pharmaceuticals, or at negative temperatures for frozen foods and long-term storage. Modern systems may also include smart monitoring features, remote alerts, and AI-based temperature tracking for enhanced operational control.
Test Cases of Cold Rooms
As a trusted Cold Room Manufacturers in India, we serve businesses across various industries that meet professional visual communication requirements.
| Test Parameter | Test Method | Purpose | Result |
|---|---|---|---|
| Temperature Stability Test | Continuous Monitoring | Ensures consistent storage conditions | Pass |
| Insulation Performance Test | Thermal Retention Analysis | Verifies energy efficiency | Pass |
| Refrigeration Capacity Test | Load Simulation | Confirms cooling performance | Pass |
| Door Seal Integrity Test | Leakage Inspection | Prevents temperature loss | Pass |
| System Reliability Test | Extended Operation Evaluation | Validates continuous performance | Pass |
Features of Cold Rooms
As Cold Room Suppliers in India, we have advanced features that ensure high precision, durability, and consistent performance.
- High-Performance Insulation Manufactured using premium PUF panels that minimize heat transfer and improve cooling efficiency throughout the storage area.
- Precise Temperature Control Advanced control systems maintain accurate temperatures to support product preservation and regulatory compliance.
- Modular ConstructionThe modular design allows quick installation, future expansion, and flexible customization based on storage requirements.
- Energy-Efficient RefrigerationOptimized cooling systems reduce power consumption while delivering reliable and consistent refrigeration performance.
- Smart Monitoring Capabilities Optional AI-based temperature monitoring systems provide real-time tracking, alerts, and enhanced operational visibility.
Benefits of Cold Rooms
As Cold Room Manufacturers in India, our products provide several benefits including consistent quality, smooth finish, and long service life.
- Extended Product Shelf LifeControlled temperature conditions help preserve freshness, quality, and usability of stored products for longer periods.
- Reduced Product LossesStable cooling environments minimize spoilage, wastage, and inventory losses caused by temperature fluctuations.
- Improved Storage Capacity Cold rooms provide significantly larger storage space compared to conventional refrigeration equipment.
- Regulatory Compliance Support Accurate temperature management helps businesses comply with food safety and pharmaceutical storage standards.
- Lower Operating CostsEnergy-efficient designs reduce electricity consumption while ensuring reliable cooling performance.
Applications of Cold Rooms
As Cold Room Suppliers in India, our all types are used in various types of industrial sectors such as:
- Frozen Food Storage Frozen Food Cold Rooms maintain low temperatures required for storing frozen products, helping preserve quality, texture, and shelf life.
- Food Processing IndustryCold rooms support food manufacturers by providing controlled storage conditions for raw materials, semi-finished products, and finished goods.
- Restaurants and Hotels Cold Storage Solutions for Restaurants and Hotels help manage large inventories of ingredients while maintaining freshness and food safety standards.
- Pharmaceutical Industry Pharmaceutical Cold Rooms (+2°C to +8°C) are used to store vaccines, medicines, and healthcare products under strict temperature-controlled conditions.
- Dairy Product Storage Cold rooms preserve milk, butter, cheese, and other dairy products by maintaining consistent refrigeration temperatures.
- Fruits and Vegetables Temperature-controlled storage helps maintain freshness, nutritional value, and market quality of agricultural produce.
- Meat and Poultry StorageCold rooms provide safe storage conditions that help prevent spoilage and maintain product quality before distribution.
- Beverage Industry Manufacturers and distributors use cold rooms to store beverages at controlled temperatures before shipment and retail supply.
- Distribution and Logistics CentersCold storage facilities support temperature-sensitive inventory management throughout the supply chain and distribution process.
- Large Cold Storage Projects Facilities such as 1000 MT Cold Storage Projects utilize industrial cold rooms for bulk storage and long-term preservation of products.
Why Choose Us?
- Customized Cold Storage Solutions We design cold rooms according to specific storage capacities, temperature ranges, and industry requirements.
- Advanced Refrigeration Expertise Our team provides efficient refrigeration systems engineered for reliable cooling performance and long-term operation.
- Premium Construction Quality We use high-quality PUF panels, refrigeration components, and durable materials for superior system reliability.
- End-to-End Project Support From design and installation to commissioning and maintenance, we provide complete project assistance.
- Reliable Service and Maintenance Our dedicated support team ensures smooth operation through timely maintenance and technical service solutions.
Choose H. A. Engineering is leading Cold Room Manufacturers and Suppliers in India. We provide advanced Cold Rooms designed to deliver reliable temperature-controlled storage for food, pharmaceutical, agricultural, and industrial applications. Whether you require a Walk-In Cold Storage Room, Modular Cold Room, Frozen Food Cold Room, or a specialized Pharmaceutical Cold Room, our systems are engineered to ensure product safety, operational efficiency, and long-term performance. By combining energy-efficient refrigeration technology, durable insulated construction, and intelligent monitoring solutions, we help businesses protect valuable inventory while optimizing storage operations. Contact Us For More Details.
FAQs
A cold room is a temperature-controlled storage area that uses refrigeration systems and insulated panels to maintain specific cooling conditions for stored products.
The ideal temperature depends on the product being stored. Fresh products typically require temperatures between 0°C and 8°C, while frozen products may require temperatures below -18°C.
A modular cold room is built using prefabricated insulated panels that allow easy installation, relocation, and expansion compared to traditional construction methods.
Ammonia is often preferred for large industrial systems due to its efficiency, while Freon-based systems are commonly used in commercial applications because of easier operation and maintenance.
Yes, modern cold rooms can incorporate AI-based temperature monitoring systems that provide real-time data, alerts, and remote performance tracking.