Milk Processing Plant
Milk Processing Plant Manufacturers in India
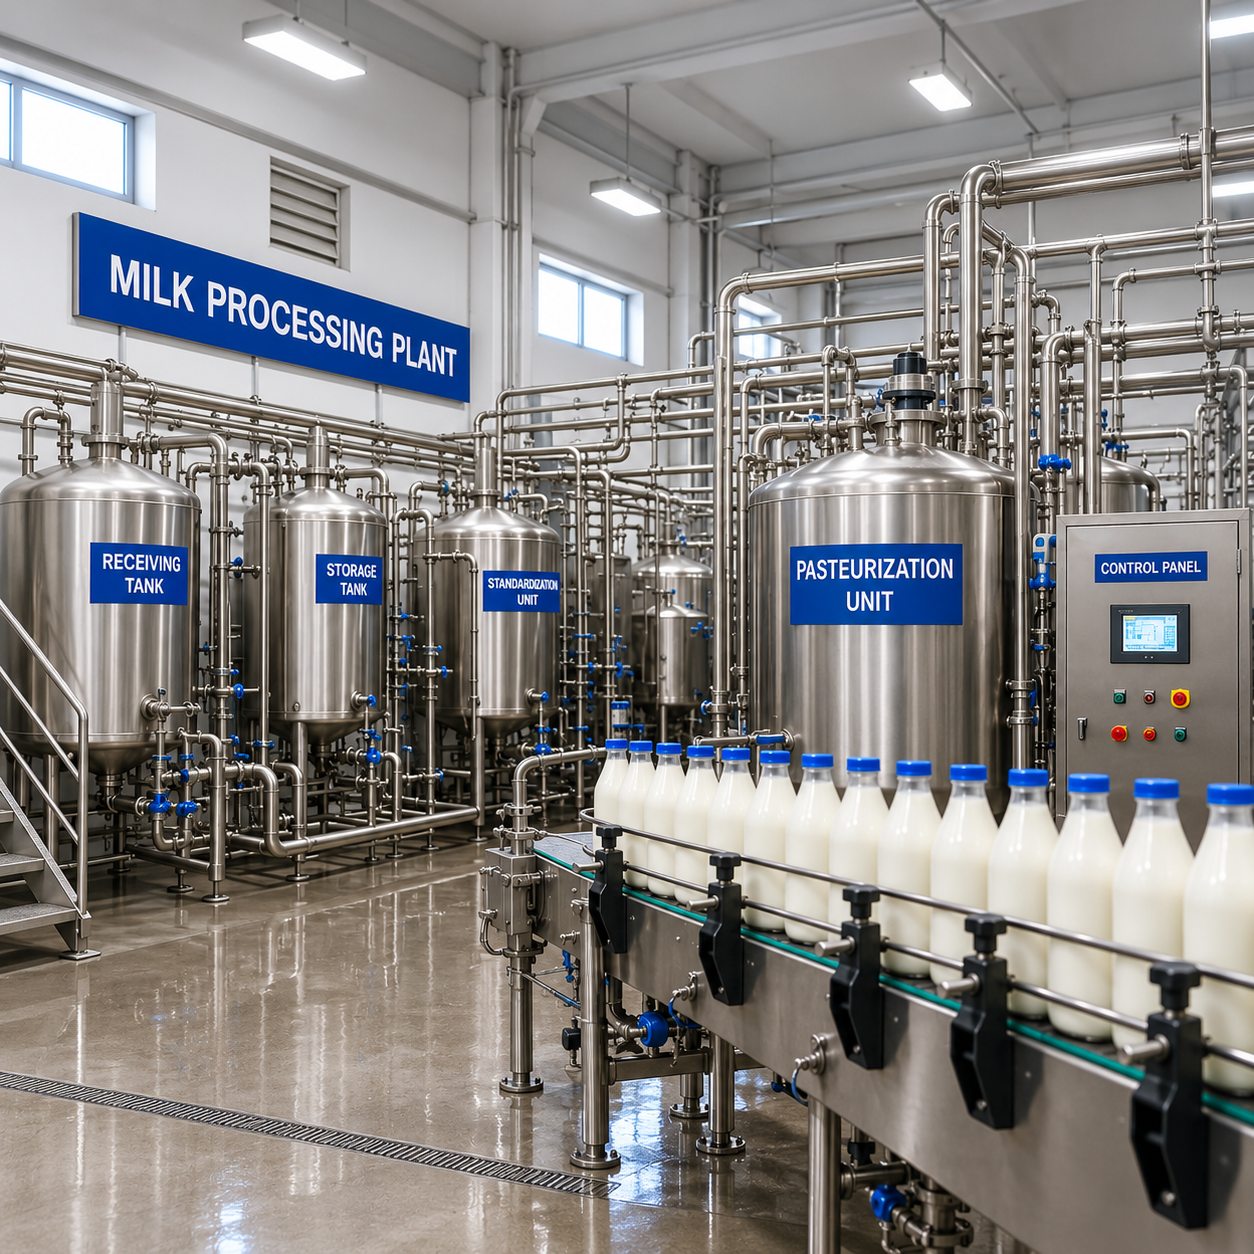
H. A. Engineering is leading Milk Processing Plant Manufacturers and Suppliers in India. We specialize in designing and manufacturing advanced Milk Processing Plants that help dairy businesses increase production capacity, improve operational efficiency, and maintain strict quality standards.
Our expertise covers the complete dairy processing chain, enabling businesses to transform raw milk into a diverse range of value-added products such as pasteurized milk, toned milk, double toned milk, full cream milk, flavored milk, yogurt, butter, cheese, ghee, and other dairy products.
We provide complete turnkey solutions including plant design, engineering, manufacturing, installation, automation, and after-sales support. Whether you require a Mini Milk Processing Plant, 5000 LPH Milk Processing Plant, 10000–50000 LPH Plant, or a 100000 LPD Dairy Plant, we deliver customized systems that align with your production goals and future expansion plans.
What is a Milk Processing Plant?
A Milk Processing Plant is an integrated facility that transforms raw milk into safe, hygienic, and market-ready dairy products through a series of controlled processes. The plant utilizes specialized machinery for receiving, filtering, chilling, pasteurizing, homogenizing, storing, and packaging milk while maintaining strict quality standards.
Modern dairy plants are designed to improve productivity, reduce manual handling, and ensure consistent product quality. Depending on production requirements, a milk processing plant can manufacture various dairy products including pasteurized milk, toned milk, full cream milk, skimmed milk, yogurt, butter, cheese, ghee, flavored milk, and UHT milk.
Equipment Used in Milk Processing Plants
- Milk Reception Tank
- Raw Milk Storage Tank
- Milk Chilling System
- Plate Heat Exchanger (PHE)
- Milk Pasteurizer Plant
- Homogenizer
- Cream Separator
- CIP Cleaning System
- Milk Packaging Machine
- Refrigeration System
- Milk Evaporation Plant
- Condensed Milk Processing System
Working Process of a Milk Processing Plant
- Raw milk is collected and received at the plant.
- Quality testing and filtration are performed.
- Milk is chilled and temporarily stored.
- Pasteurization eliminates harmful microorganisms.
- Homogenization ensures uniform fat distribution.
- Milk is standardized according to product specifications.
- Packaging is completed using automated systems.
- Finished products are stored and dispatched.
How Much Land Is Required for a Milk Processing Plant?
The land requirement depends on plant capacity, product range, utility infrastructure, storage facilities, and future expansion plans. Small processing plants generally require less space, while large-scale dairy processing units need extensive production and storage areas.
What Is the Cost of Setting Up a Dairy Plant?
The cost of a dairy processing plant varies depending on capacity, automation level, product range, utility requirements, and plant configuration. Turnkey projects involving complete engineering, processing equipment, packaging systems, and installation generally require higher investment compared to basic processing setups.
Test Cases of Milk Processing Plants
As a trusted Milk Processing Plant Manufacturers in India, we serve businesses across various industries that meet professional visual communication requirements.
| Test Parameter | Test Method | Purpose | Standard | Result |
|---|---|---|---|---|
| Pasteurization Performance Test | Temperature Verification | Ensure milk safety | Dairy Industry Standards | Pass |
| Homogenization Test | Fat Distribution Analysis | Maintain product consistency | Quality Standards | Pass |
| CIP Cleaning Test | Hygiene Inspection | Validate cleaning efficiency | Food Safety Standards | Pass |
| Production Capacity Test | Output Monitoring | Verify plant performance | Design Specifications | Pass |
| Packaging Integrity Test | Seal Quality Inspection | Prevent contamination | Industry Compliance | Pass |
Features of Milk Processing Plants
As Milk Processing Plant Suppliers in India, we have advanced features that ensure high precision, durability, and consistent performance.
- Integrated Dairy Processing System: Our milk processing plants combine multiple operations including chilling, pasteurization, homogenization, storage, and packaging within a single streamlined system. This integrated approach improves production efficiency and simplifies plant management.
- Fully Automated Plant Operations: Advanced automation technology continuously monitors critical processing parameters to ensure consistent product quality. Automated controls reduce manual intervention, improve productivity, and minimize operational errors.
- Hygienic Stainless Steel Construction: All equipment is manufactured using premium-grade stainless steel that meets dairy industry hygiene requirements. The corrosion-resistant construction ensures safe product handling and long-term operational reliability.
- Flexible Production Capabilities: The plant can process various dairy products including pasteurized milk, toned milk, flavored milk, yogurt, butter, cheese, and ghee. This flexibility allows businesses to expand their product portfolio and increase profitability.
- Scalable Capacity Options: We offer milk processing plants ranging from 50 LPH to 5000 LPH, 10000 LPH to 50000 LPH, and 100000 LPD Dairy Plants. Customized capacities are available to match current production requirements and future growth plans.
Benefits of Milk Processing Plants
As Milk Processing Plant Manufacturers in India, our products provide several benefits including consistent quality, smooth finish, and long service life.
- Supports Business Expansion: A modern milk processing plant enables dairy businesses to increase production capacity and enter new market segments. The ability to manufacture multiple dairy products creates opportunities for revenue growth and market expansion.
- Enhances Product Quality: Advanced processing technologies ensure milk and dairy products maintain consistent taste, texture, nutritional value, and safety standards. This helps strengthen brand reputation and customer trust.
- Improves Production Efficiency: Automated systems reduce manual labor requirements and streamline production workflows. This results in higher productivity, reduced downtime, and improved utilization of resources.
- Enables Product Diversification: The plant allows manufacturers to produce a wide range of dairy products from a single facility. Diversification helps businesses respond to changing consumer preferences and market demand.
- Delivers Long-Term Returns: Investing in a milk processing plant provides sustainable operational benefits through improved efficiency, reduced wastage, and higher production output. This contributes to long-term profitability and business stability.
Applications of Milk Processing Plants
As Milk Processing Plant Suppliers in India, our all types are used in various types of industrial sectors such as:
- Pasteurized Milk Production: Milk processing plants are extensively used for producing pasteurized milk that meets food safety regulations and consumer expectations. Proper processing ensures safe and hygienic milk for daily consumption.
- Toned and Double Toned Milk Manufacturing: The plant enables precise standardization of milk fat content to produce toned and double toned milk products. These products are widely consumed due to their balanced nutritional profile.
- Full Cream Milk Processing: Processing systems help maintain the rich texture and nutritional value of full cream milk while ensuring product consistency. Advanced equipment supports efficient large-scale production.
- Flavored Milk Production: Milk processing plants are ideal for manufacturing flavored milk products with consistent quality and taste. The process supports the addition of flavors, nutrients, and other ingredients.
- Yogurt Manufacturing: Specialized processing systems facilitate controlled fermentation and production of high-quality yogurt products. This helps manufacturers meet growing consumer demand for healthy dairy options.
- Cheese Production: The plant provides the necessary processing conditions for producing various cheese varieties. Consistent milk quality contributes to better yield, texture, and product performance.
- Butter and Ghee Manufacturing: Milk processing facilities support efficient cream separation and fat processing for butter and ghee production. Advanced equipment improves product quality and manufacturing efficiency.
- UHT Milk Processing: Ultra-high-temperature processing systems enable the production of long shelf-life milk products suitable for large-scale distribution. This expands market reach and storage flexibility.
- Organic and A2 Milk Processing: Dedicated processing lines can be configured for premium dairy segments such as organic milk and A2 milk. This helps businesses serve specialized consumer markets effectively.
- Cooperative Dairy Operations: Milk processing plants support cooperative societies by processing milk collected from multiple farmers. These facilities strengthen dairy supply chains and improve overall operational efficiency.
Why Choose Us?
- Leading Dairy Processing Equipment Manufacturer: We have extensive experience in manufacturing advanced milk processing plants for diverse dairy industry applications. Our expertise enables us to deliver reliable and efficient processing solutions.
- Complete Turnkey Project Solutions: From plant design and engineering to installation and commissioning, we provide comprehensive turnkey project services. This ensures seamless project execution and faster operational readiness.
- Customized Plant Design: Every dairy business has unique production goals and operational requirements. We develop customized plant configurations that maximize efficiency, productivity, and future scalability.
- High-Quality Engineering Standards: Our processing equipment is manufactured using premium materials and advanced engineering techniques. This guarantees durability, performance, and compliance with industry standards.
- Dedicated Technical Support: We provide ongoing technical assistance, maintenance support, and operator training to ensure smooth plant operations. Our commitment to customer service helps maximize plant performance throughout its lifecycle.
Choose H. A. Engineering is well known Milk Processing Plant Manufacturers and Suppliers in India. A well-designed Milk Processing Plant is more than just a production facility—it is a strategic investment that enables dairy businesses to expand product offerings, improve operational efficiency, and strengthen their market presence. By integrating advanced technologies for pasteurization, homogenization, chilling, storage, and packaging, modern dairy plants help transform raw milk into high-quality products that meet consumer expectations and industry standards. We are committed to delivering innovative and reliable Milk Processing Plant Solutions that support long-term business success. Contact Us For More Details.
FAQs
Milk processing plants typically include milk reception tanks, pasteurizers, homogenizers, storage tanks, PHE systems, refrigeration units, CIP systems, and packaging machines.
The land requirement depends on plant capacity, utility infrastructure, storage needs, and future expansion plans. Larger plants require additional space for production and logistics operations.
The cost varies based on plant capacity, automation level, processing technology, and project scope. Turnkey dairy projects generally involve higher investment than basic processing facilities.
The ideal manufacturer offers high-quality equipment, customized engineering solutions, turnkey project support, and dependable after-sales service for long-term operational success.
Milk processing plants are available in capacities ranging from 50 LPH to 5000 LPH, 10000 LPH to 50000 LPH, and 100000 LPD Dairy Plants for large-scale dairy operations.